About Conveyor Belt
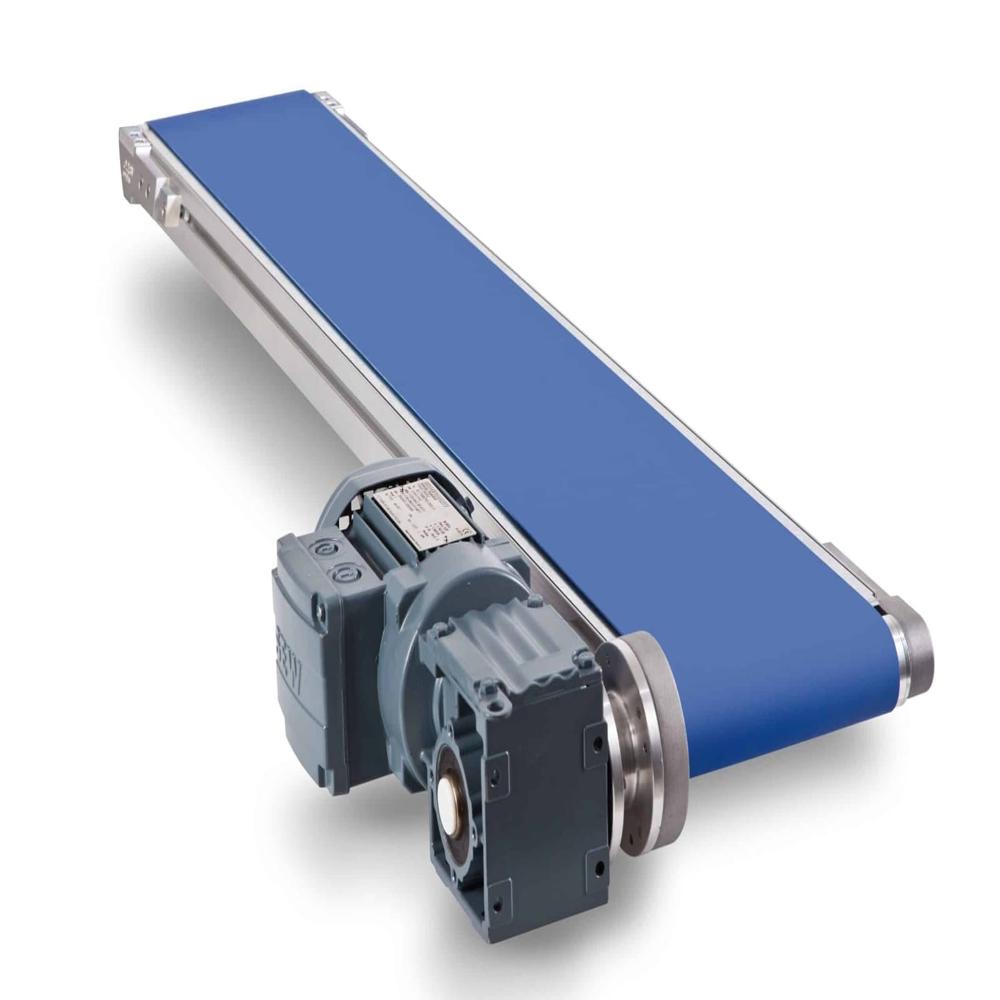
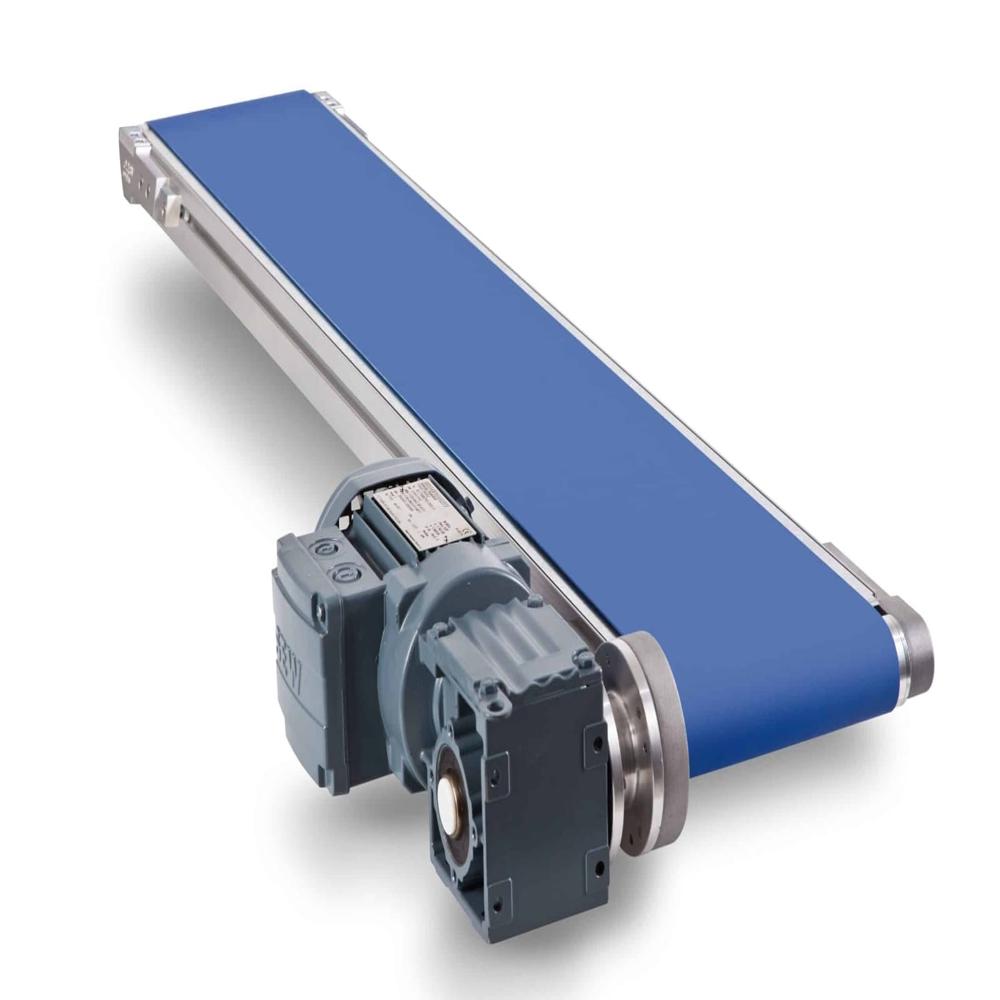
Conveyor belts are continuous material-handling systems designed to transport goods, products, and bulk materials efficiently from one location to another. They are widely used in manufacturing, warehouses, mining, food processing, packaging, and logistics industries for reliable and cost-effective material movement.
Customizable and Durable DesignEngineered for flexibility, this conveyor accommodates a wide range of operational needs with customizable lengths, widths, and belt colors. Its oil and chemical resistance ensures reliable performance in diverse environments, while the robust aluminum frame and sealed bearings offer lasting durability with minimal maintenance.
Smooth and Quiet OperationWith a noise level below 65 dB and a speed range of 0.1 to 2 m/s, the conveyor delivers efficient, gentle transport of materials. The powder-coated or anodized finish provides extra resistance to wear, enhancing both the aesthetics and lifespan of the unit.
FAQ's of Conveyor Belt:
Q: How is the conveyor belt installed and can it be moved after setup?
A: The conveyor is primarily floor-mounted for stability, but portable options are available for easy relocation if your workspace layout changes.
Q: What applications are best suited for this conveyor model?
A: This conveyor is ideal for material handling, packaging lines, and assembly processes, especially where cleanliness and low noise are crucial.
Q: When should I choose a customized size for the belt and length?
A: Custom widths (300 mm - 1200 mm) and lengths (1 m - 20 m) are best selected when your application demands a specific conveyor footprint, ensuring optimal fit and efficiency in your facility.
Q: Where is this conveyor typically deployed within industrial settings?
A: Common installation sites include warehouses, production floors, packaging zones, and assembly lines within manufacturing and logistics sectors.
Q: What is the process for maintaining the conveyor?
A: Routine maintenance involves inspecting the belt's surface, checking sealed ball bearings, and ensuring proper motor function. The oil and chemical-resistant materials facilitate easy cleaning and upkeep.
Q: What are the main benefits of using this conveyor?
A: Key advantages include reliable, smooth material transport, noise reduction, easy maintenance, and strong resistance to oils and chemicals, ensuring consistent performance and safety.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS


